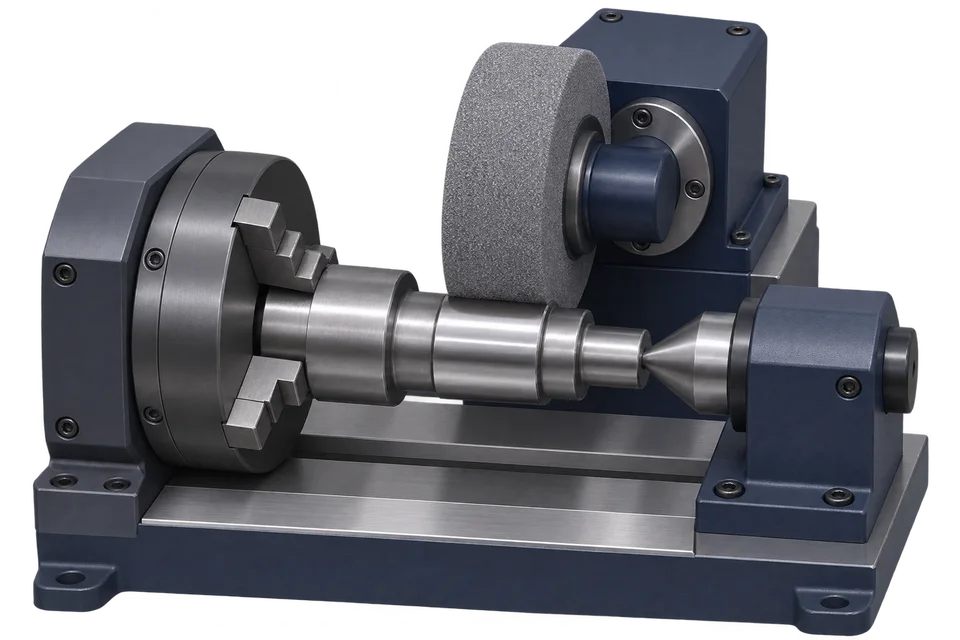
Cylindrical grinding time formula
For external cylindrical grinding, the approximate removal volume is the circumference times the ground length times the radial allowance. Multiply the specific removal rate Q′w in mm³/(mm · s) by the effective engagement width in mm to get the material removal rate.
Calculate roughing and finishing separately using their own stock allowance and Q′w. Add approach, spark-out, clamping and handling to get cycle time.
Grinding time in min = removal volume ÷ (Q′w × effective width) ÷ 60
Worked example for external cylindrical traverse grinding
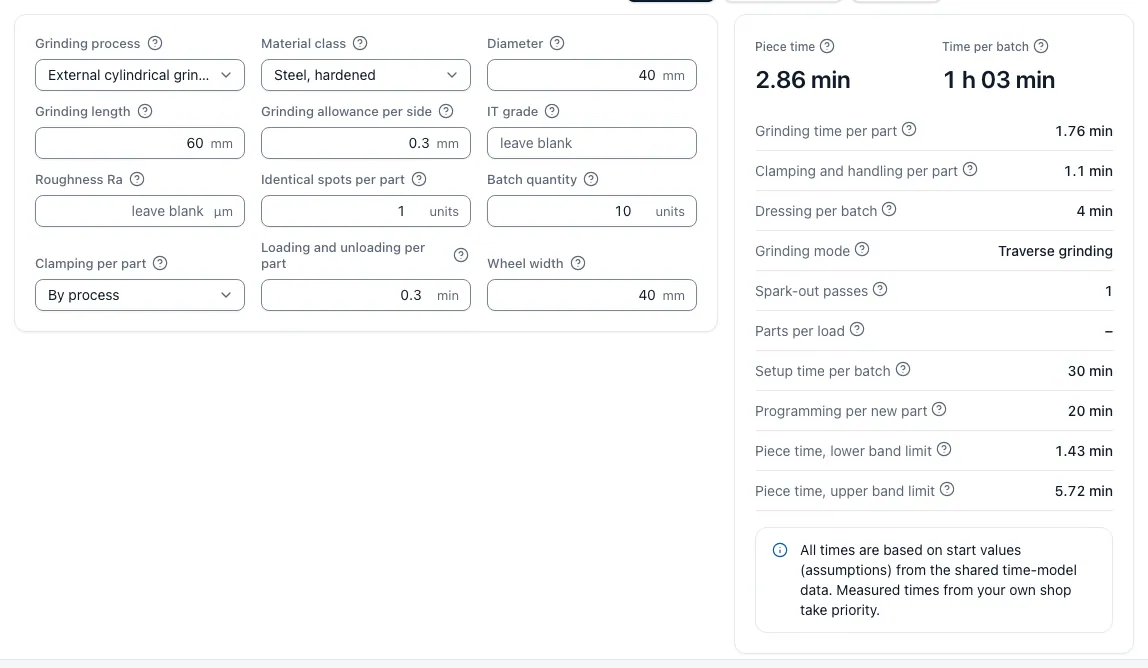
A hardened bearing journal is 40 mm in diameter and has a 60 mm grinding length. The example uses a radial allowance of 0.30 mm, IT6 and Ra 0.4 µm. With a 40 mm wheel and a 20 mm effective width, the app selects traverse grinding.
Using the app's starting values, one journal takes about 1.88 min per part including approach and spark-out. The example allows zero additional clamping, loading and unloading time. Dressing, setup and programming are shown separately.
Time components for one bearing journal
| Time share | Time |
|---|---|
| Scraping | 1.1310 min |
| Arbitration | 0.4712 min |
| Spark-out | 0.1800 min |
| Approach | 0.1000 min |
| Cycle time for the example part | 1.8822 min |
These are planning estimates. Use measured shop times when available.
Estimate surface grinding by chuck load and quantity
Surface grinding time per load depends on allowance, infeed, crossfeed strokes, how the parts are arranged and table feed. Parts that fit on the same chuck share the table runs. A partially filled final load needs its own run.
Dressing time depends on the interval specified for the grinding wheel. Enter a measured cycle time for double-disc grinding and centreless plunge grinding. The app adds the estimated batch times.
Sources and classification
- Grinding time in the CNC Kalkulator app
Model and starting values for cylindrical and surface grinding.
Questions and answers
Is grinding allowance measured radially or on the diameter?
Cylindrical grinding uses the radial allowance. To remove 0.60 mm from the diameter, enter a radial allowance of 0.30 mm. For surface grinding, enter the allowance per ground face.
What is spark-out in grinding?
After the last infeed, the wheel makes further passes without advancing. Allow time for these passes to achieve the required dimensions and finish.