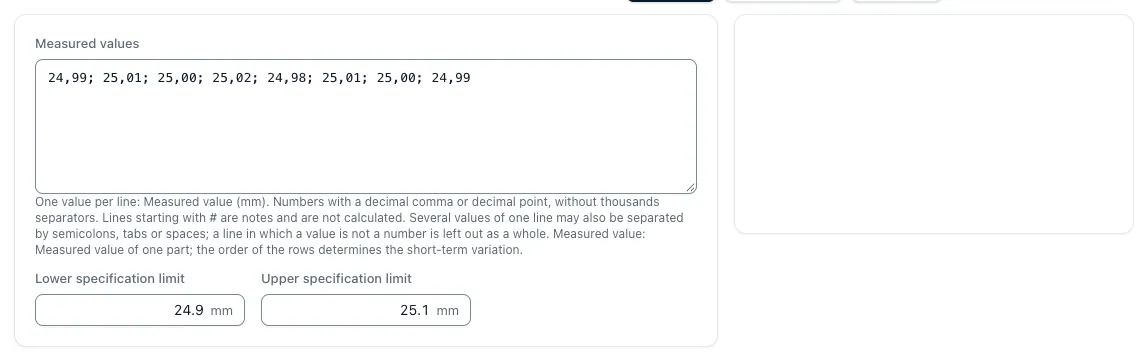
Use measured values in chronological order
The sequence determines the sliding spans between adjacent individual measurements. A sorting by size would change this structure and can make the short-term scatter appear artificially small. All values must concern the same measurement size and comparable process conditions.
Lower and upper specification limits are product requirements. They are not derived from the largest and smallest measured values.
Separating short-term and total scattering
For Cp and Cpk, the app estimates the short-term standard deviation with a mean moving span divided by 1,128. Pp and Ppk, on the other hand, use the sample standard deviation of the entire input series.
Cp alone does not evaluate the centering. Cpk uses the smaller distance from the mean to one of the specification limits. A process close to a limit can therefore have an unfavourable Cpk despite a wide tolerance.
σ_abbreviated = MR̄ the 1,128; Cp = (USL − LSL) the (6 × σ_abbreviated); Cpk = min(USL − Mean, Mean, Mean, LSL) the (3 × σ_abbreviated)
Short calculation example of the formula
The sequence 24,99; 25,01; 25,00; 25,02; 24,98; 25,01; 25,00; 24,99 mm has the mean value of 25,00 mm. The average sliding span is 0.02 mm. This follows σ_short ᐅ 0.017730 mm.
With specification limits 24,90 and 25,10 mm, Cp = Cpk = 1,880. The total standard deviation is approximately 0,013093 mm, so Pp = Ppk ᐅ 2,546. The eight values serve only for comprehensible calculation and are not sufficient proof of ability.
Ability requires a suitable process and data
Process stability, distribution form, appropriate measurement and a representative sufficient sample must be checked outside this simple calculation. The computer does not perform a complete stability or normality test.
No unlimited capability can be derived from identical measured values. If the scatter used is zero, the corresponding index remains undetermined. Modelled ppm outside the limits are also not actually counted error parts.
Sources and classification
- NIST: Process Capability
Definition and requirements of Cp and Cpk.
- NIST: Individual Control Charts
Estimation of short-term dispersion from successive individual values and sliding spans.
Questions and answers
May I sort the readings before entering them?
No, if the short-term scatter is to be estimated over sliding spans. This requires the chronological order of measurement.
Which Cpk is sufficient?
The required value is derived from the valid agreement and the appropriate detection method. A standard limit value does not replace this requirement or the verification of stability and data basis.