

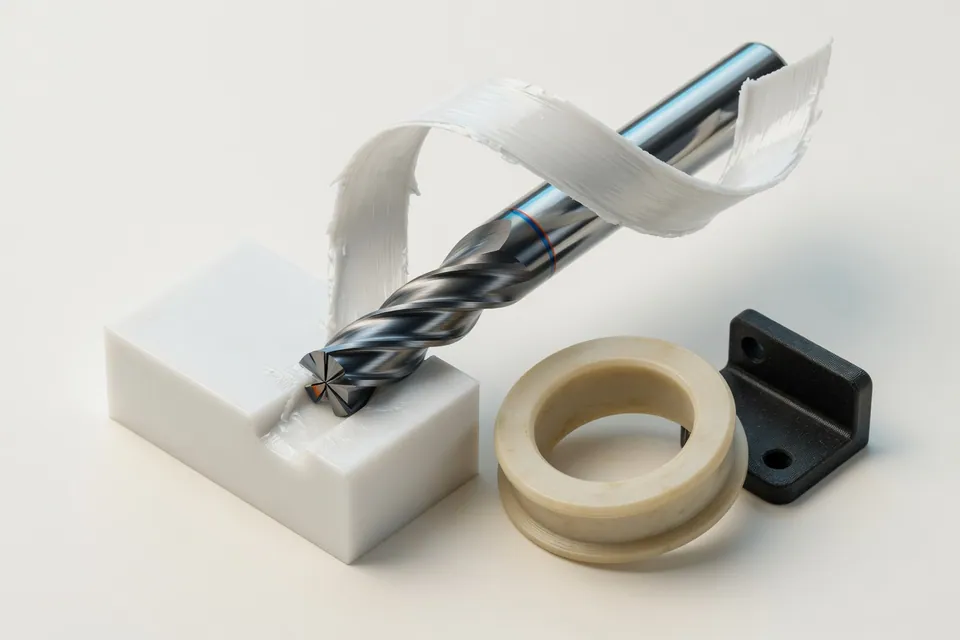
Plastics in the cut data finder
The cutting data finder of the app leads four plastics with their own value ranges: POM-C (Polyacetal), PA 6 (Polyamide 6), PEEK (Polyether ether ketone) and PE-HD. They are located outside the ISO groups P to H in a separate group of plastics. The specific cutting force kc1.1 is 200 to 350 N/mm² at a fraction of the values for steel; cutting force and drive power therefore rarely limit machining.
According to the app's material database, the elasticity module is between 1 GPa (PE-HD) and 3.7 GPa (PEEK), while for steel it is 210 GPa. A plastic part is more resistant to clamping and cutting forces. In addition, high thermal expansion, moisture absorption with polyamide and internal stresses in the semi-finished product are added.
Start values for POM-C, PA 6, PEEK and PE-HD
The areas come from the cut data finder of the app; the starting value is the centre of the range, the tooth feed applies to a 10 mm diameter cutter, the drilling feed for a 10 mm drill. The information provided by the tool and semi-finished products manufacturer is binding.
At 450 m/min, a milling machine with a 10 mm diameter needs around 14,300 1/min. If the spindle limit is below this, cutting data for milling machines will calculate with the maximum speed and accordingly reduce cutting speed and feed speed; 12,000 1/min are pre-set.
- POM-C: milling vc 300–600 m/min, fz 0.08–0.20 mm; turning vc 300–600 m/min, f 0.10–0.40 mm; drilling vc 100–300 m/min, f 0.10–0.30 mm
- PA 6: milling vc 250–500 m/min, fz 0.08–0.20 mm; turning vc 250–500 m/min, f 0.10–0.40 mm; drilling vc 100–250 m/min, f 0.10–0.30 mm
- PEEK: milling vc 200–400 m/min, fz 0.06–0.15 mm; turning vc 200–400 m/min, f 0.10–0.30 mm; drilling vc 80–200 m/min, f 0.08–0.20 mm
- PE-HD: milling vc 300–600 m/min, fz 0.10–0.25 mm; turning vc 300–600 m/min, f 0.10–0.40 mm; drilling vc 100–300 m/min, f 0.10–0.30 mm
Thermal expansion and dimensional stability
Plastics expand by many times more than metals when heated. The app expects the following expansion coefficients: PE-HD 180, POM-C 110, PA 6 90 and PEEK 47 μm/(m·K), for comparison C45 11,5 and EN AW-6082 23,4 μm/(m·K).
A 100 mm long measure changes by 0.18 mm at 10 K temperature difference for PE-HD, 0.11 mm at POM-C, 0.09 mm at PA 6 and 0.047 mm at PEEK; 0.012 mm at C45. If you measure and measure a POM part heated by cutting immediately, you will find it after cooling out of a tolerance of a few hundredths. The heat expansion calculator of the app calculates this change linearly; at large temperature ranges and near softening the approximation is not loadable.
ΔL = L₀ × α × ΔT
Moisture, voltages and fibre reinforcement
PA 6 absorbs moisture and changes its dimensions; the app recommends measuring after storage. PEEK is high-quality and expensive, stresses in the semi-finished product are degraded by tempering before finishing. PE-HD is soft and needs large chip spaces and sharp cutting. POM-C is very well machined, with narrow tolerances the thermal expansion remains the critical point.
Fiberglass reinforced grades such as PA 6-GF30, PA 66-GF30 and PEEK-GF30 are listed in the app's catalogue of materials with its own density; for cutting data, it refers to the unreinforced base material. The fiberglasses are abrasive, the app advises on carbide or diamond tools. For these grades, calculate with shorter service life than the base material.
CFRP laminates are only available in the catalogue with density: 1.55 g/cm³ quasiisotropic, 1.58 g/cm³ unidirectional. The app does not provide cutting data for this purpose. The information in the catalogue: carbon fibers are abrasive, their dust is conductive, diamond tools and extraction are necessary. The cutting values come here exclusively from the tool manufacturer.
Calculation risks for plastic parts
The main time is rarely the cost driver for plastic. In a comparison cutter Ø 10 mm, three cutting edges, 10 mm cutting depth and 5 mm cutting width, the starting values for POM-C on a spindle with 12,000 1/min around 250 cm³/min, for PEEK around 150 cm³/min; C45 comes in the same case at 46 cm³/min.
Expensive plastic parts are placed elsewhere: in semi-finished products, especially in PEEK, in tensioners that do not deform the soft part, in intermediate steps such as tempering or bearings before the finished dimension, in measurement after temperature balancing and in reject, when a measure after cooling no longer fits. These positions belong individually in the calculation.
The raw weight of the app calculates the stored density, for example 1,41 g/cm³ for POM-C, 1,32 g/cm³ for PEEK, 1,14 g/cm³ for PA 6, 1,36 g/cm³ for PA 6-GF30 and 0,95 g/cm³ for PE-HD.
Questions and answers
Which cutting speed applies to POM during milling?
The cutting data finder of the app lists for POM-C 300 to 600 m/min with starting value 450 m/min and a tooth feed of 0.08 to 0.20 mm for a 10 mm diameter milling machine. For small milling machines, the spindle speed is usually limited.
Does the app deliver cut data for CFRP?
No. CFRP laminates are found in the density material database of the app and indicate abrasive fibers, conductive dust, diamond tools and extraction. The app does not specify its own cutting values; the information provided by the tool manufacturer is decisive.
How much does a POM measure change during cooling?
The extension coefficient of the app of 110 μm/(m·K) changes a 100 mm long measure at 10 K by 0.11 mm. The heat expansion calculator calculates this for your length and temperature difference; the linear approximation does not apply near the softening.
What changes with PA 6-GF30 compared to PA 6?
The app's material database runs PA 6-GF30 with 1.36 instead of 1.14 g/cm³ and refers to PA 6 for cutting data.The glass fibers are abrasive; the app advises on carbide or diamond tools, while the service life is shorter than the unreinforced base material.

